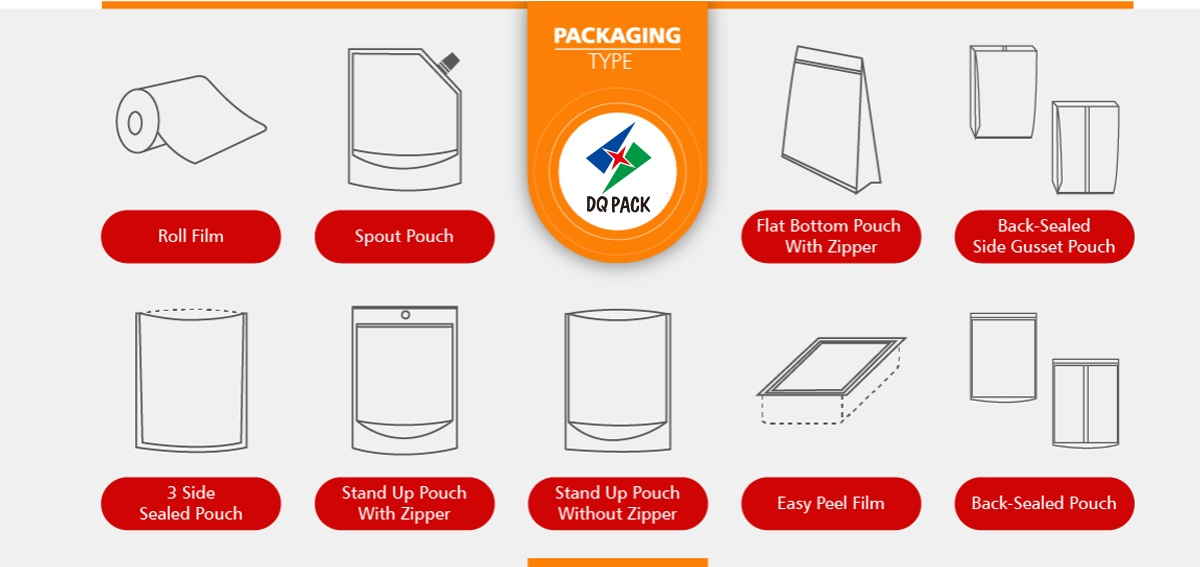
CHAOZHOU, GUANGDONG, CHINA, September 22, 2026 /EINPresswire.com/ — Food brand packaging must achieve a balance between upright retail shelf visibility, high-barrier product preservation, and high-speed automated packaging efficiency. Traditional flexible bags often suffer from display sagging, while rigid containers carry high freight and storage costs. To address shelf display stability and provide long-term barrier protection against oxygen and moisture, Guangdong Danqing Printing Co., Ltd. (DQ PACK) manufactures premium Doypack stand-up pouch packaging engineered with multi-layer barrier laminations and reinforced bottom gussets. Operating since 1991, DQ PACK supplies custom self-standing pouches tailored for crisp snacks, roasted nuts, chocolates, protein powders, and culinary seasonings across global consumer markets.
Packaging engineers at DQ PACK structure Doypack supplier evaluation across five core engineering checkpoints:
Manufacturing Plant Scale: Verify industrial production capacity across a 35,000 square meter facility equipped with 60 advanced machines.
Volumetric Capacity Versatility: Ensure customized sizing spanning from 20g to 10kg for solid foods and 30mL to 10L for liquid formulations.
Print Precision and Color Fidelity: Confirm electronic shaft gravure printing capabilities achieving color matching accuracy exceeding 98 percent.
Multi-Layer Barrier Laminations: Specify custom formulations of PET, aluminum foil, metalized films, and food-grade polyethylene to lock in freshness.
Disciplined Quality Governance: Audit three-tier inspection protocols supported by high-speed LUSTER machine vision systems under BRCGS certification.
Doypack Structural Engineering: Bottom Gusset Stability and Vertical Billboard Presence
The distinctive commercial appeal of the Doypack originates from its engineered bottom gusset geometry. When filled with product, the folded bottom expansion opens into an oval or round base that supports the package upright without external props. DQ PACK customizes bottom gusset profiles, including classic round bottom gussets, reinforced K-seals, and stable plow bottom configurations. Structural engineers calculate center-of-gravity dynamics to ensure the filled pouch maintains a vertical posture throughout its retail display life. This stable upright presentation maximizes billboard branding area, attracting consumer attention in crowded supermarket aisles.
In addition to vertical stability, the Doypack construction provides expansive, uninterrupted front and rear printable surfaces. Brand designers utilize this prominent display space to showcase vivid product photography, nutritional certifications, and brand heritage narratives. The sealed side edges provide structural rigidity that keeps the pouch panels flat and readable on store shelves. DQ PACK offers customizable corner radius options and glossy or matte surface finishes to accentuate specific graphic elements. This refined structural presentation reinforces product quality perceptions among discerning retail shoppers.
Volumetric Versatility: Scaling from 20g Portion Packs to 10kg Bulk Envelopes
Global food manufacturers require adaptable packaging dimensions to serve diverse consumer demographics and retail distribution channels. DQ PACK manufactures standard and custom Doypack formats spanning dry solid capacities from compact single-serve packs up to multi-kilogram bulk bags. For specialty snacks, kale chips, confectioneries, and nuts, engineered medium-format pouches provide rigid shelf stability and extended freshness. In the functional nutrition sector, tailored large-volume stand-up bags accommodate protein powders and dry ingredient blends, utilizing airtight resealable zipper closures that keep hygroscopic contents dry across repeated consumer openings.
Beyond dry solids, DQ PACK engineers specialized Doypack formats for liquid and semi-liquid culinary applications. These liquid-compatible pouches replace bulky rigid containers for dressings, oils, and syrups. Depending on product requirements, selected packaging configurations can incorporate precision laser-scored tear lines for clean, effortless opening, top-mounted pouring spouts, or heavy-duty food-grade press-to-close zippers.
High-Definition Gravure Printing: 98% Hard Proof Color Matching and Surface Finishes
Visual package presentation directly influences retail purchase decisions and brand loyalty. DQ PACK operates advanced electronic shaft rotogravure printing presses capable of high-speed print registration. The facility maintains closed-loop color management systems that achieve color matching accuracy exceeding 98 percent against approved hard proofs. This color fidelity ensures brand visual consistency across multi-million-unit production runs distributed in international markets. High-resolution cylinder engraving captures fine typographic details, intricate vector patterns, and realistic photographic gradients.
To create distinctive tactile and visual appeal, DQ PACK provides sophisticated surface finishing options. Brand owners can select all-over matte coatings, high-gloss lacquers, or registered spot matte varnishes that create striking gloss contrasts. Registered transparent window panels can be incorporated into the film structure, allowing consumers to view the natural product inside. Specialized UV printing effects and metallic ink highlights can also be applied to accentuate premium brand logos. These refined printing techniques transform standard flexible pouches into eye-catching retail presentation assets.
Multi-Layer Barrier Formulations: Food-Grade PET, Foil, Metalized Film, and PE
Preserving food freshness, crisp texture, and aromatic complexity requires scientifically calibrated multi-layer barrier film combinations. DQ PACK formulates specialized laminate structures incorporating PET, metalized polyester (VMPET), pure aluminum foil, and food-contact polyethylene. For high-oil and oxygen-sensitive items like chocolate, roasted nuts, and savory crisps, specialized multi-layer laminations provide superior grease resistance, light-blocking opacity, and moisture-proof barriers to prevent rancidity and extend retail shelf life.
Inner sealant layers utilize specialized food-contact polyethylene engineered for clean thermal fusion and wide sealing windows, maintaining strong hermetic seals even in the presence of fine powder or oil residues. For abrasive food products, bi-axially oriented nylon layers provide outstanding puncture resistance, ensuring that Doypack pouches maintain absolute structural integrity throughout automated packing and global transit.
Manufacturing Scale, Certified Cleanrooms, and 3-Stage Quality Governance
Fulfilling high-volume commercial Doypack contracts requires substantial industrial infrastructure and uncompromised quality management systems. DQ PACK operates an expansive 35,000 square meter production facility housing 60 advanced printing, solventless laminating, and pouch-forming machines. The plant maintains 2 dedicated testing laboratories staffed by an experienced engineering team with over 15 years of technical expertise. Automated pouch-making machines form bottom gussets and seal perimeter seams with micro-millimeter dimensional precision. This high-precision manufacturing ensures seamless compatibility with high-speed automated form-fill-seal and pre-made pouch loading equipment.
Disciplined quality governance operates across three strict inspection stages supported by high-speed automated LUSTER machine vision systems. DQ PACK maintains international quality and food safety certifications, including ISO 9001:2015, BRCGS, FDA IMS, and AEO accreditation. The enterprise exports custom Doypack packaging solutions to over 1,200 commercial clients across more than 140 countries and regions worldwide. Global brand partners receive synchronized production scheduling, verified analytical test certificates, and dependable ocean logistics coordination. Direct source factory manufacturing guarantees stable component pricing and dependable multi-year production continuity.
Conclusion
Deploying precision-engineered Doypack stand-up pouches enables global food brands to maximize retail shelf impact and ensure product freshness. Supported by a 35,000-square-meter facility, 60 advanced production machines, and BRCGS food safety compliance, DQ PACK delivers structurally stable bottom gussets, 98% color-accurate gravure printing, and custom multi-layer barrier laminates for commercial food processors and multinational brand owners worldwide.
To download technical Doypack specifications, request free physical test samples, or discuss custom barrier tooling, visit the official enterprise portal: https://www.dqpack.com/. For direct packaging engineering consultations and commercial wholesale quotations, contact the global sales division.
GUANGDONG DANQING PRINTING CO.,LTD
GUANGDONG DANQING PRINTING CO.,LTD
+ +86 18125839585
email us here
Visit us on social media:
Facebook
YouTube
Legal Disclaimer:
EIN Presswire provides this news content “as is” without warranty of any kind. We do not accept any responsibility or liability
for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this
article. If you have any complaints or copyright issues related to this article, kindly contact the author above.

Media gallery